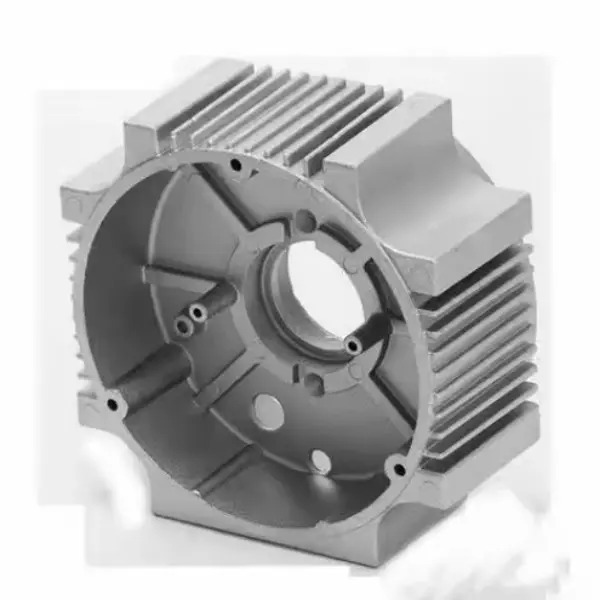
Real projects, real results. Explore how Sunmy has helped OEMs, engineering teams, and product developers across Europe and North America bring their designs to life — from complex CNC machined parts and precision turning to stamped components, castings, and injection-molded assemblies.
Each case study shows the challenge, the process, and the outcome — including how we handled material selection, tolerances, surface finishing, and quality verification with CMM and FAI.
Have a similar project? Send us your drawings or samples — let’s build it together.
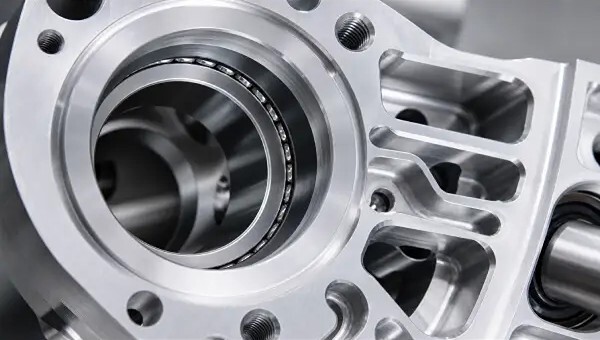
The client’s initial iterations suffered from unacceptable kinematic backlash during high-velocity trajectory reversals. Root cause analysis traced this to a 0.045mm coaxiality deviation between the opposing planetary gear bearing bores, primarily induced by stack-up errors from multiple workpiece repositionings in standard 3-axis machining. Furthermore, aggressive material removal (over 75% volume reduction to achieve the webbed lightweight topology) released immense residual stresses, causing a 0.08mm geometric warpage across the main mounting flange and leading to IP67 seal failures in the field.
Our Solution
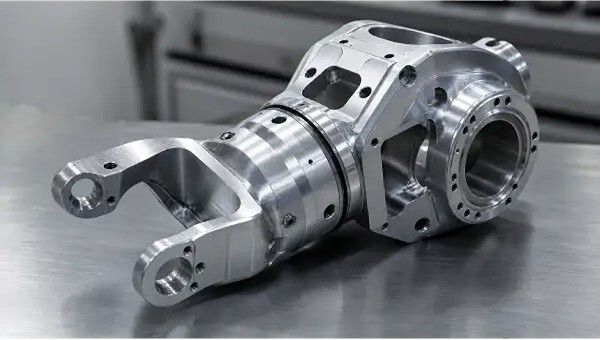
Sunmy Hardware engineers intercepted the drawing and mandated the use of 7075-T651 (stress-relieved) aluminum billet. We overhauled the CAM strategy to introduce a controlled thermal stress-relief bake cycle strictly between the heavy roughing and micro-finishing toolpaths. Utilizing our HAAS 5-axis CNC machining centers, we executed the final interpolation of all critical bearing journals, dowel pin indexing holes, and mating surfaces in a single, uninterrupted setup. To combat chatter on the 1.5mm thin-wall deep pockets, we engineered custom low-frequency vibration-dampening workholding fixtures.
Result
The single-setup 5-axis protocol successfully held a 0.008mm coaxiality and 0.012mm true position across the bearing bores, directly eliminating joint backlash. Post-machining warpage was reduced to zero, yielding a perfectly planar flange that passed the client’s strict 100-bar pneumatic leak test and 5-million cycle dynamic load validation.